
CPNF Standardized Integrated System
Equipment Applications
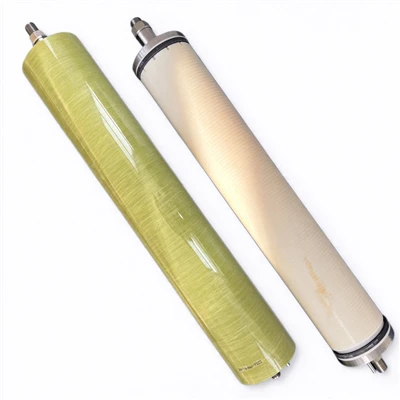
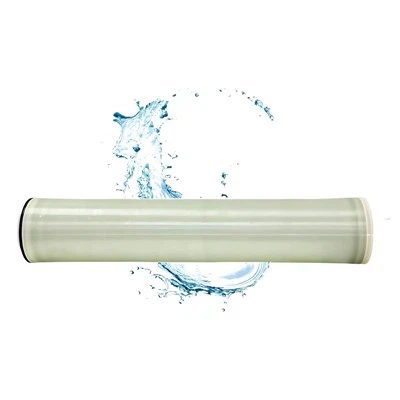
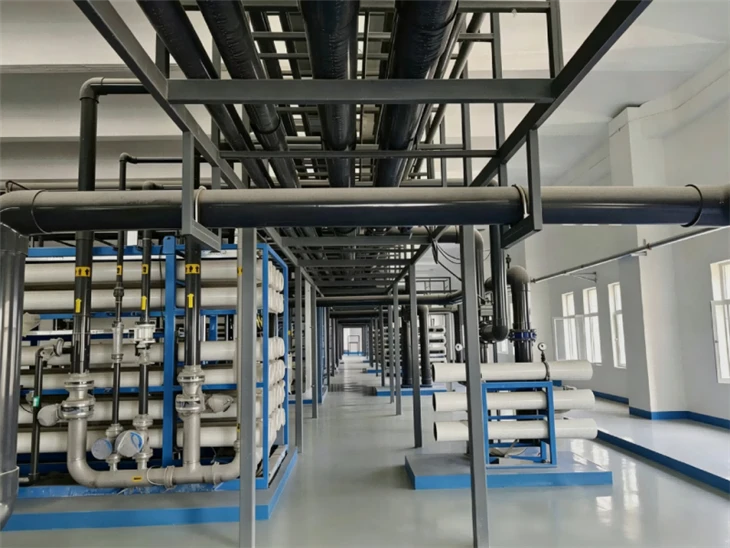
CPNF High-pressure Nanofiltration Integrated Unit is a high-performance specialty NF system for selective ion fractionation and feed purification. Fitted with specially coated imported NF sheets, it delivers excellent divalent ion rejection, stable permeate quality, and resistance to high pressure shock and frequent chemical cleaning. It is widely used for chlor-alkali denitrification, coal chemical & coking wastewater, mine brine recovery, salt lake Li-Mg separation, industrial feed purification and ZLD salt separation. Featuring modular skid-mounted design, it is highly automated, compact and easy to maintain. Custom skid or containerized systems are offered to fit various water conditions.
Equipment Parameters
|
Serial No. |
Parameter |
Unit |
50m³/d (permeate) |
100m³/d (permeate) |
150m³/d (permeate) |
|
1 |
Single Membrane Area |
m2 |
34 |
34 |
34 |
| 2 |
Differential Membrane Pressure |
Bar/unit |
0.3~0.8 | 0.3~0.8 | 0.3~0.8 |
|
3 |
Membrane Quantity |
Unites |
15 | 30 | 75 |
|
4 |
Recovery Rate |
% |
50~80 | 50~80 | 50~80 |
|
5 |
Floor Space (skid mounted) |
L*W*H |
7*1.5*2.5 | 7*1.8*2.5 | 7*2.0*2.5 |
| 6 |
Floor Space (container type) |
L*W*H |
6*2.4*2.8 | 9*2.4*2.8 | 9*2.4*2.8 |
Case Study

Guizhou Chlor-Alkali Denitrification Project
- Core Objective: Treat saline wastewater from denitrification process for advanced treatment and reuse
- Overall Plant Design Capacity: 1900 m³/h (including pretreatment system + advanced treatment system) NF
- Treatment Capacity: 80 m³/h(NF)
- Design Recovery Rate: 75%
- Operating Pressure: 30 bar
- Total Membrane Elements: 80 pcs
- Process Flow: Pretreatment → Ceramic Membrane → Chelating Resin → Nanofiltration → Reverse Osmosis Outcome: It rejects divalent sulfate ions. The stable permeate can be reused as make-up water for the denitrification system and process water for chlor-alkali production.
About Us
In Integrated Solutions
As one of reliable China DTRO Module 75bar manufacturers, we produce high-pressure disc tube RO modules with octagonal diversion discs and corrosion-resistant FRP pressure vessels.
We can flexibly adjust the system's heat resistance level and automatic disinfection cycles according to customers' production shifts and actual working temperature ranges.


Hot Tags: CPNF Standardized Integrated System, China CPNF Standardized Integrated System manufacturers, suppliers, factory, Disc Tube Reverse Osmosis, dtro, high pressure membrane, high pressure membrane concentrate management module, high pressure membrane pressure vessel module, High Pressure Reverse Osmosis