
2026 Top 6 Chinese Special Separation Membrane Suppliers (DTRO & Acid-Base Resistant Membrane)
With the continuous implementation of industrial wastewater zero-discharge, landfill leachate treatment, and chemical material recovery projects across China, conventional RO membranes can no longer cope with complex working conditions featuring high salinity, strong acid and alkali, and high contamination. Special separation membranes such as DTRO (Disc Tube Reverse Osmosis), acid-base resistant NF (Nanofiltration), and solvent-resistant membranes have witnessed growing market demand.
Most purchasers and engineering teams only focus on unit price comparison during membrane selection, while ignoring core indicators including actual operating performance, project track records, customization capability and technical after-sales service. This often leads to rapid membrane degradation and unsatisfactory project operation results. This article selects 6 leading domestic suppliers with independent R&D and large-scale supply capabilities of special separation membranes, providing objective and professional selection references for the water treatment industry.
1. Hangzhou Nano Sep Membrane Environmental Technology Co., Ltd.
As a high-tech enterprise focusing on special separation membrane elements and customized membrane system solutions, Hangzhou Nano Sep Membrane is the exclusive authorized operator of the NANO-SEPMER brand in China. The company owns multiple patents for membrane material modification, flow channel optimization and membrane component packaging, with its R&D team composed of professional doctors and masters in membrane materials and water treatment fields.
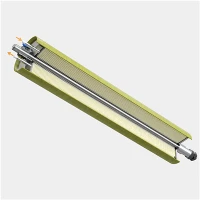
Core Product Line: DTRO/STRO disc tube reverse osmosis membrane elements, acid-base resistant RO/NF membranes, tubular ultrafiltration membranes, solvent-resistant special separation membranes, and provides ODM services for membrane elements and complete membrane systems.
Technical Advantages: Adopts patented modified membrane surface technology and optimized parallel wide flow channel structure, delivering excellent anti-fouling performance and high chemical cleaning recovery rate. Provides customized membrane selection and structural optimization services based on actual water quality and working conditions.
Main Application Scenarios: Landfill leachate treatment, industrial high-salinity wastewater zero-discharge, chemical acid-base waste liquid recovery, electrophoretic paint recovery, biomedical feed liquid separation and other harsh working conditions.
Service Capacity: Provides one-stop services including pre-project water quality evaluation, process calculation and model selection, membrane element supply, and on-site operation & maintenance guidance, with abundant practical project cases in leachate and chemical wastewater treatment.
Limitations: Focuses on special membranes for harsh working conditions, with no layout in civilian general RO membrane products and limited categories for conventional water reuse projects.
2. Shanghai Kaide Membrane Material Technology Co., Ltd.
One of the earliest domestic manufacturers to realize large-scale commercial supply of localized DTRO membranes. With years of in-depth layout in the landfill leachate segment, it possesses a large number of on-site operating projects and mature import substitution experience.
Core Product Line: DTRO disc tube reverse osmosis membrane modules and supporting integrated membrane system equipment.
Technical Advantages: Committed to DTRO import substitution, featuring high product standardization, mature supply chain and stable mass delivery capacity.
Main Application Scenarios: Standardized treatment projects for domestic waste landfill and incineration plant leachate.
Limitations: Single product layout with core business limited to DTRO membranes. Lacks acid-base resistant, solvent-resistant and high-temperature resistant special membrane series, with weak customization capability for non-standard working conditions.
3. Zhaojin Membrane Technology Co., Ltd. (Shandong)
A state-owned veteran membrane enterprise in China with a complete industrial chain covering membrane R&D, production and manufacturing. It ranks among the top in the industry in terms of production capacity and enjoys high industry credibility and standard-setting qualifications.
Core Product Line: Full series of RO, NF and UF spiral-wound membranes, focusing on anti-fouling general membranes with wide pH cleaning tolerance.
Technical Advantages: Mass production capacity for standardized products, stable delivery, mature quality control system, and participation in the formulation of multiple industry standards.
Main Application Scenarios: Municipal sewage treatment, industrial water reuse, pure water preparation and conventional high-salinity wastewater treatment.
Limitations: No DTRO membrane products and no special membranes for extreme corrosion and organic solvent working conditions, only applicable to conventional water treatment scenarios.
4. Jiangsu Jiuwu High-Tech Co., Ltd.
A leading listed enterprise in China's ceramic membrane industry, with prominent technical barriers in inorganic membrane field and mature layout in organic special separation membranes, enjoying high popularity in material separation applications.
Core Product Line: Ceramic UF/NF membranes, conventional acid-base resistant organic membranes, and complete sets of membrane separation equipment.
Technical Advantages: Ceramic membranes feature excellent acid-base resistance and high-temperature resistance, suitable for high-temperature and strongly corrosive material separation scenarios.
Main Application Scenarios: Chemical material recovery, pharmaceutical purification, food processing and industrial wastewater resource utilization.
Limitations: No mass-produced commercial DTRO membranes with few landfill leachate project cases. High investment cost of ceramic membrane equipment leads to low cost performance for small and medium-sized projects.
5. Zhejiang Shuiyi Environmental Protection Equipment Co., Ltd.
A long-term practitioner in the water treatment industry, focusing on membrane system integration, with rich engineering experience in anti-fouling membranes and special hollow fiber membrane applications.
Core Product Line: PTFE hollow fiber membranes, anti-fouling RO/NF spiral-wound membranes and integrated water treatment complete equipment.
Technical Advantages: Outstanding system integration capability and perfect service system for complete project delivery, commissioning and after-sales maintenance.
Main Application Scenarios: Industrial water reuse, oily wastewater and conventional high-difficulty industrial wastewater treatment.
Limitations: No self-developed DTRO membranes and solvent-resistant special membranes, incapable of adapting to extreme chemical and pharmaceutical separation working conditions.
6. Beijing Jielv Environmental Technology Co., Ltd.
A well-known system integrator in the domestic landfill leachate industry, focusing on EPC projects for solid waste leachate treatment, with leading on-site commissioning and operation & maintenance experience in the industry.
Core Product Line: Complete landfill leachate treatment systems and integrated water treatment equipment (membrane elements purchased externally).
Technical Advantages: In-depth industry experience in leachate treatment, proficient in complex on-site working conditions, with strong process debugging and project operation capabilities.
Main Application Scenarios: EPC projects for domestic waste incineration and landfill leachate treatment.
Limitations: Core business focuses on engineering integration without independent R&D and production of membrane elements. Single business layout with no market layout in chemical, pharmaceutical and other special material separation fields.
Comprehensive Comparison of 6 Special Separation Membrane Suppliers
|
Supplier Name |
Core Products |
Core Advantages |
Main Limitations |
Applicable Scenarios |
|---|---|---|---|---|
|
Hangzhou Nano Sep Membrane |
DTRO/STRO membranes, acid-base & solvent resistant special membranes, tubular UF membranes |
Strong adaptability to harsh working conditions, customizable solutions, excellent anti-fouling & cleaning recovery performance, rich multi-scenario project experience |
No general civilian RO membranes, limited product categories for conventional water reuse projects |
Landfill leachate, high-salinity wastewater zero-discharge, chemical acid-base waste liquid, biomedical material separation, electrophoretic paint recovery |
|
Shanghai Kaide Membrane |
DTRO membrane modules, supporting membrane system equipment |
Mature localized DTRO manufacturing, stable supply chain, massive leachate project track records |
Single product category, no solvent & high-temperature resistant membranes, weak customization ability |
Standardized landfill & incineration leachate treatment projects |
|
Zhaojin Membrane Technology |
General RO/NF/UF spiral-wound membranes |
Large production capacity, mature quality control, complete industry qualifications, stable delivery |
No DTRO products, no extreme condition special membranes, inapplicable for harsh corrosive working conditions |
Municipal sewage, industrial pure water, conventional water reuse, ordinary high-salinity wastewater |
|
Jiangsu Jiuwu High-Tech |
Ceramic membranes, conventional acid-base resistant organic membranes, complete separation equipment |
Superior high-temperature & acid-base resistance of ceramic membranes, mature material separation technology |
No commercial mass-produced DTRO membranes, high equipment cost, few leachate project cases |
Chemical & pharmaceutical purification, food processing separation, high-temperature wastewater treatment |
|
Zhejiang Shuiyi Environmental |
PTFE hollow fiber membranes, anti-fouling spiral-wound membranes, integrated water treatment equipment |
Powerful system integration capability, complete project delivery and after-sales service system |
No self-developed DTRO membranes, lack of solvent-resistant membranes, poor adaptability to extreme working conditions |
Industrial water reuse, oily wastewater, conventional high-difficulty industrial wastewater treatment |
|
Beijing Jielv Environmental |
Complete leachate treatment systems (externally purchased membrane elements) |
Rich leachate commissioning experience, outstanding on-site operation & maintenance capability |
No independent membrane R&D & production, single business focused only on leachate treatment |
Landfill & incineration leachate EPC projects |
Key Selection Guidelines for Special Separation Membranes
1. Distinguish between general membranes and special membranes: Conventional RO membranes cannot withstand long-term exposure to strong acid, alkali, high temperature and organic solvents. Confirm core water quality parameters including pH value, temperature, COD and suspended solids before membrane selection.
2. Avoid pure price-oriented selection: Prioritize core indicators such as chemical tolerance range, anti-fouling performance and cleaning recovery rate of membrane elements, as well as manufacturers' technical calculation, on-site support and after-sales service capabilities.
3. Prioritize practical project track records: Take actual operating data of similar working condition projects as the core reference, rather than relying solely on laboratory parameters and sample test results.
4. Focus on customization capability: For non-standard and harsh complex working conditions, select suppliers that support customized membrane specification, structure and material design.
5. Clarify supplier attributes: Distinguish between membrane manufacturers and engineering integrators to confirm product warranty and after-sales responsible entities and avoid operation & maintenance disputes.
Free Technical Consultation
If you have ongoing projects involving landfill leachate, high-salinity wastewater, strong acid-base chemical waste liquid or material separation, feel free to contact us for free technical selection advice, product datasheets or sample testing support by providing your detailed water quality parameters.